Bucket Elevators
Bucket elevators are material handling systems designed for inclined and vertical conveying of bulk materials. They are used across a wide range of industries, from mining to food processing.
Learn More ↓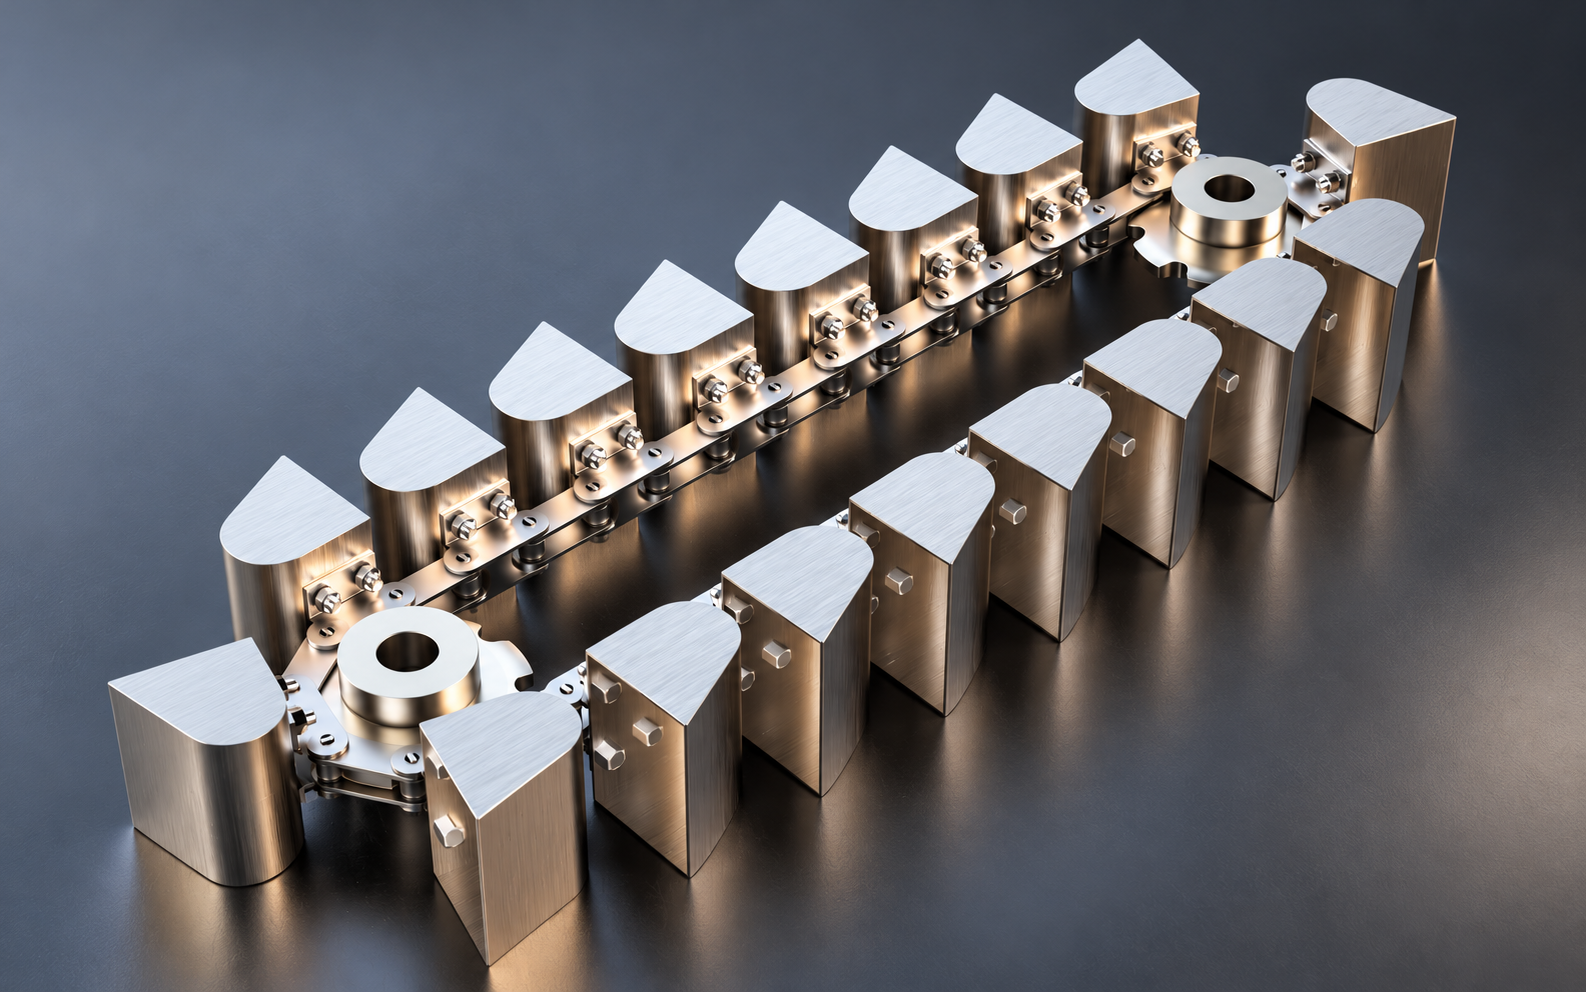
Vertical Conveying of Bulk Materials
Bucket elevators can operate as standalone units or as components of larger conveying and processing systems.
Vertical Conveying
Reliable conveying of free-flowing and bulk materials between different elevations within the production process.
Buckets and Traction Elements
For abrasive and coarse-grained materials, designs with buckets attached to a chain or conveyor belt are used.
Customised Design
Conveying capacity, lifting height and material properties determine the structure, drive system and selection of the elevator’s operating components.
Engineered for Capacity and Material Requirements
Bucket elevators are used either as standalone equipment or as part of conveying systems of various sizes. For abrasive and coarse-grained materials, the buckets are mounted on a chain serving as the traction element, while belt-mounted buckets are used for free-flowing and less abrasive materials.
Our bucket elevator range is based on standardised, carefully selected core components, including traction elements, drive assemblies and tensioning systems.
Key factors in selecting the appropriate bucket elevator type include capacity, the material being conveyed and the required conveying distance.
These parameters determine the most suitable design to meet the required operating function.
Bucket Elevator Installations
Examples of PROMID bucket elevator installations, structural details and operating components.
Have Questions?
Need advice, a quotation or a technical solution? Get in touch with us.