Chain Conveyors with Rubber Belts
Chain conveyors with rubber belts are material handling systems designed for transporting bulk materials. They are particularly suitable for demanding operating conditions and material handling in recycling and processing plants.
Learn more ↓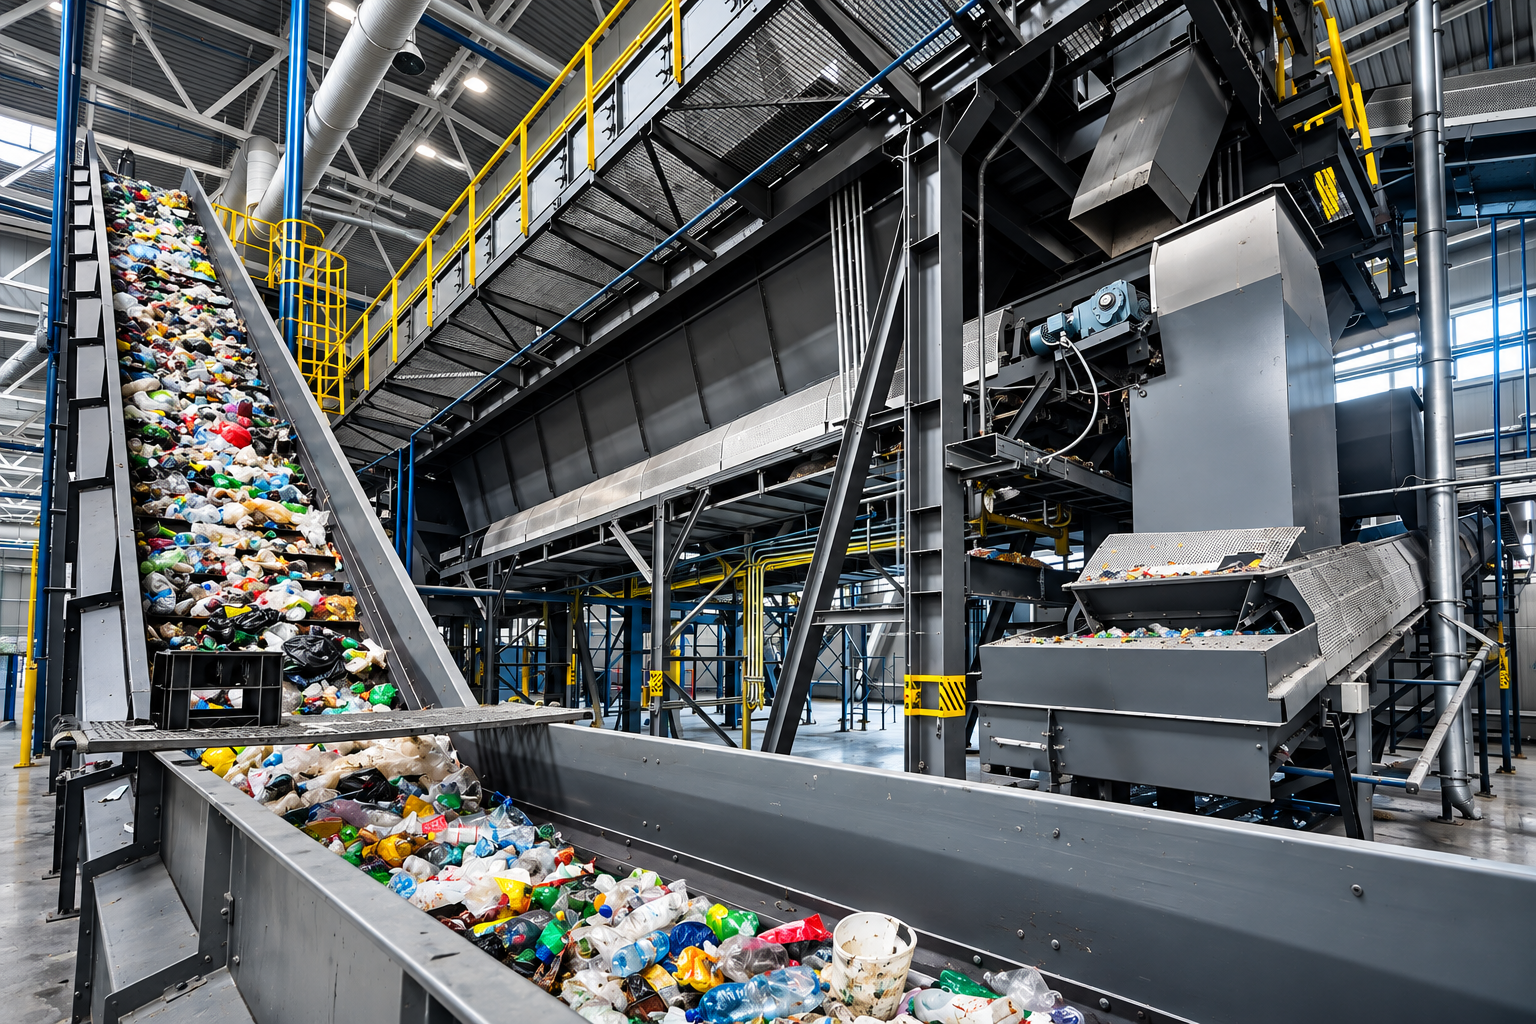
Transport of Bulk and Waste Materials
Conveyor design is determined by the type of material, required capacity, operating conditions, and the length of the conveying route.
Demanding Operating Conditions
The robust design is suitable for material handling in facilities with high mechanical loads and demanding operating conditions.
Bulk Material Handling
The system enables continuous conveying of various types of bulk materials and waste throughout the production process.
Plant-Specific Design
The conveyor’s main dimensions are defined according to the conveying route, type of material, and specific plant requirements.
Robust Design for Continuous Conveying
Chain conveyors with rubber belts are used to transport bulk materials. The material is typically fed into and accumulated in a feed hopper, then conveyed by the belt to the next stage of the process.
The type of chain conveyor with a rubber belt is selected according to the material being handled and other technical and process-related conveying requirements.
The conveyor’s overall dimensions are determined by the conveying route and customer requirements, with the supporting structure, drive assembly, and conveyor belt adapted accordingly.
This design is particularly suitable for recycling systems, waste sorting facilities, and other processes requiring reliable, continuous conveying of different types of materials.
Project Examples
Examples of chain conveyors with rubber belts and conveying lines used for recycling and processing waste materials.
Have a Question?
Need advice, a quotation, or a technical solution? Get in touch with us.